Customer BackgroundNovaCore Electronics Manufacturing Ltd. is an electronics manufacturing comp
WhatsApp : +86 15601902607
Email : info@qinsun-lab.com
NovaCore Electronics Manufacturing Ltd. is an electronics manufacturing company headquartered in the Republic of Alves. The company specializes in the research and development and production of precision electronic components, industrial control modules, and portable electronic devices.
As its export business continues to expand, the company has begun extending its operations into the fields of avionics components, outdoor electronic equipment, and high-altitude applications. During transportation, storage, and actual use, these products may be exposed to low-pressure environments. Therefore, it is necessary to simulate different atmospheric pressure conditions to evaluate their performance stability and structural reliability under low-pressure conditions.
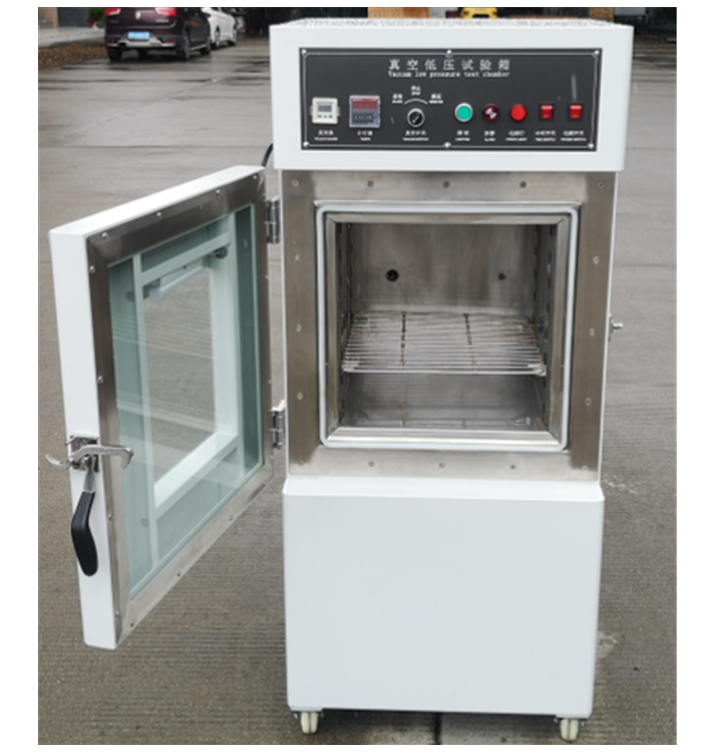
To strengthen its internal quality inspection system, NovaCore decided to purchase a Vacuum Low Pressure Test Chamber for product development verification, batch quality control, and new product reliability assessment. After comprehensively evaluating the equipment's functions, technical configuration, and after-sales support capabilities, the customer ultimately selected the Vacuum Low Pressure Test Chamber supplied by our company.
Before purchasing the equipment, NovaCore primarily relied on external testing agencies for low-pressure environmental testing. Although this approach met some of its testing requirements, the increasing number of product models and testing tasks gradually revealed several challenges.
Long External Testing Lead Times
For each low-pressure test, the customer had to book testing resources in advance and coordinate sample transportation and testing schedules. The resulting waiting time affected product development progress and increased project management costs.
Limited Flexibility in Adjusting Test Conditions
Different electronic products have different requirements for test pressure, test duration, and testing procedures. Relying on external laboratories made it difficult for the R&D team to adjust test conditions promptly according to the specific characteristics of each product.
Increasing Product Quality Verification Requirements
As the company's export markets expanded, the customer needed to establish more comprehensive internal testing procedures to identify potential problems before products left the factory and reduce the risk of malfunctions during transportation and use.
Lack of Continuous Testing Data
Records from multiple external testing sources made it more difficult to organize and compare test data. This also limited engineers' ability to analyze product performance across different batches, structural designs, and testing conditions.
Therefore, the customer sought to introduce reliable, controllable, and user-friendly vacuum low-pressure testing equipment to improve its in-house environmental simulation testing capabilities.
To address NovaCore's actual requirements, our company recommended the Vacuum Low Pressure Test Chamber to simulate low-pressure environments and help the customer establish a more standardized product testing process.
During project implementation, we communicated with the customer regarding sample dimensions, testing objectives, target pressure range, test duration, and equipment installation conditions. Based on the final confirmed technical requirements, we provided the corresponding equipment configuration.
After installation and commissioning were completed, our technical personnel assisted the customer with operational training, covering the following key areas:
Test Parameter Configuration: Setting the target pressure, test duration, and other relevant operating parameters according to product testing requirements.
Testing Procedure Operation: Guiding the customer through test preparation, equipment startup, monitoring during testing, and procedures following test completion.
Sample Testing Procedures: Assisting the customer in establishing procedures for sample placement, pre-test inspections, and post-test condition assessments.
Routine Maintenance Training: Explaining equipment cleaning, sealing component inspections, and routine checks of operating conditions.
Test Record Management: Helping the customer standardize the recording of test conditions and sample status to facilitate subsequent quality analysis and traceability.
Through this solution, the customer gradually established an internal low-pressure environmental verification process centered on in-house testing, providing more convenient testing conditions for product development and quality management.
The Vacuum Low Pressure Test Chamber provides a controllable low-pressure simulation environment for electronic products and related components by regulating the air pressure inside the test chamber. Based on the customer's actual application requirements, the equipment offers the following advantages.
Low-Pressure Environment Simulation
The equipment can establish low-pressure test conditions in accordance with the confirmed technical specifications, helping the customer evaluate product performance under specified low-pressure environmental conditions.
Support for Testing Multiple Types of Samples
Depending on the chamber's effective working space, load capacity, and specific configuration, the equipment can be used to test electronic components, industrial control modules, portable electronic devices, and other suitable samples.
Greater Flexibility in In-House Testing
The customer can schedule testing tasks according to product development plans, reducing routine dependence on external testing resources and allowing greater flexibility in design verification and quality inspections.
Standardized Testing Procedures
By standardizing test parameters, operating procedures, and data recording methods, the customer can manage testing processes for different products and batches more effectively.
Support for Product Reliability Assessment
In conjunction with pre-test and post-test visual inspections, functional checks, and the customer's specified evaluation criteria, the equipment can help engineers identify potential abnormalities under low-pressure conditions and provide reference data for product design improvements.
After installation and commissioning, NovaCore began incorporating vacuum low-pressure testing into the internal verification procedures for selected electronic products. The R&D team gained greater flexibility in scheduling tests and was able to conduct further product analyses based on the test results.
It should be noted that the specific testing range, pressure accuracy, depressurization rate, and temperature and humidity conditions are subject to the actual equipment configuration and the technical parameters confirmed by both parties.
Through this equipment procurement and installation project, the customer improved its ability to address key requirements for low-pressure environmental testing.
Problem 1: Inflexible Testing Schedules
Solution and Results: The customer gained in-house low-pressure testing capabilities and could schedule tests according to R&D and quality inspection plans, reducing time constraints caused by external testing appointments.
Problem 2: Lack of Consistent Management of Test Conditions
Solution and Results: By standardizing parameter settings and operating procedures, the customer could carry out testing tasks in a more systematic manner and improve comparability between different tests.
Problem 3: Difficulty in Identifying Potential Product Risks in a Timely Manner
Solution and Results: Incorporating low-pressure environmental verification into product development and quality control procedures helped engineers identify abnormal product performance under specific test conditions and conduct further investigations into the underlying causes.
Problem 4: Fragmented Test Records and Difficult Traceability
Solution and Results: The customer established a more systematic test record management approach, making it easier to organize sample information, test conditions, and inspection results and providing a basis for subsequent quality improvement.
Overall, the project helped NovaCore strengthen its low-pressure environmental testing capabilities and align its testing activities more closely with its internal R&D and quality management requirements.
After the equipment was put into operation, NovaCore's quality engineering team conducted an internal evaluation of its practical application.
The customer's project manager commented:
"Before introducing the Vacuum Low Pressure Test Chamber, some of our low-pressure tests depended on external testing resources. We can now schedule relevant tests more flexibly according to our R&D progress and manage test parameters and records in a consistent manner. This has made our product verification and quality control activities more convenient."
The customer also noted that clear operational training and routine maintenance guidance helped the team become familiar with the equipment's operating procedures more quickly. Looking ahead, the company plans to further refine its low-pressure environmental testing procedures in response to new product development requirements and gradually expand the equipment's application across suitable product categories.
This project not only provided the customer with equipment for low-pressure environmental simulation testing but also supported the establishment of a more standardized internal testing process.
By continuously optimizing testing plans, standardizing operating procedures, and strengthening test data management, NovaCore Electronics Manufacturing Ltd. will further improve the systematic nature of its product verification activities and provide stronger support for quality management of electronic products intended for international markets.
Qinsun Instruments Co., LTD is a professional laboratory testing instrument manufacturer in China,Have been focusing on laboratory instrument R&D more than 30 years and have rich industry experience,Based on international testing standards,We are also the instrument supplier for BV SGS laboratory,We provide one-stop solutions for lab instruments,Free Training and Turn-Key Service,Products exported all over the world,Offer 36 month warranty and are a trustworthy partner.
Company Phone
+86-21-6420 0566
Working hours
Monday to Friday
Mobile phone:
13816217984
Email:
info@qinsun-lab.com